CNC Material Removal Rate & Horsepower Calculator
Calculate MRR (in³/min), required spindle horsepower, cutting torque, and machine utilization for milling and turning operations. Verify your machine has enough power before running aggressive cuts.
Free Tool · MRR · Spindle HP · Cutting Torque · Machine Utilization · 18 MaterialsK = specific power factor (HP·min/in³). Represents energy required to remove one cubic inch of material per minute.
Feed rate in inches per minute (IPM) for milling. Use IPR (inches per revolution) for turning.
Typical: 75–85%. Accounts for belt/gear transmission losses.
Used to calculate cutting torque at the spindle.
| Material Removal | |
| Material | — |
| Power factor (K) | — |
| Width of cut (WOC) | — |
| Depth of cut (DOC) | — |
| Feed rate | — |
| Material removal rate (MRR) | — |
| Power & Torque | |
| Net HP at spindle | — |
| Spindle efficiency | — |
| Required motor HP | — |
| Spindle speed (for torque) | — |
| Cutting torque (in-lb) | — |
| Cutting torque (ft-lb) | — |
| Machine Assessment | |
| Machine rated HP | — |
| Machine utilization | — |
| HP headroom remaining | — |
| Assessment | — |
MRR = WOC × DOC × Feed Rate. Required HP = MRR × K (material power factor) ÷ machine efficiency. The utilization bar shows how much of your machine's rated power is being used.
How MRR and Spindle Horsepower Are Calculated
Material Removal Rate (MRR) is the volume of material removed per unit time. It directly determines how much power your machine needs to sustain a cut. Every aggressive cut that stalls a spindle, trips a drive, or breaks a tool is a power calculation that wasn't done beforehand. Use MRR to verify your machine can handle the cut before you press Cycle Start.
1 Material Removal Rate
MRR for milling is simply the product of three dimensions: how wide the cut is, how deep, and how fast the tool is moving through the material. The result is a volume per unit time.
2 Required Horsepower
Each material has a specific power factor (K) — the HP required to remove one cubic inch of that material per minute. Multiplying MRR by K gives the net cutting power at the spindle. Divide by machine efficiency to get required motor power.
3 Cutting Torque
Spindle torque is calculated from HP and RPM. High-torque cuts at low RPM (heavy roughing) may exceed spindle torque limits even when HP appears sufficient. Always check both HP and torque limits on your machine spec sheet.
4 Machine Utilization
Machine utilization tells you what percentage of the spindle's rated power is being consumed by the cut. Under 70% is safe headroom. Over 90% risks spindle trips and thermal issues in continuous cutting. Over 100% will stall or fault the drive.
MRR is the single best metric for comparing machining strategies. A 2" face mill taking 0.050" DOC at 100 IPM produces MRR = 10 in³/min. A ½" endmill taking 0.500" DOC at 40 IPM produces only MRR = 10 in³/min — identical productivity, very different tool loads. When quoting a job, calculate the total volume of material to remove and divide by your target MRR to get cycle time. If MRR × K exceeds your machine's available HP, you have two options: reduce MRR (slower cycle time, lower cost per setup) or use a larger/more powerful machine (higher cost). Knowing this before the job runs is the difference between profitable and unprofitable work.
Worked Examples
HP needed = 11.9 HP motor
Utilization: 39.5% ✓
HP needed = 16.5 HP motor
Utilization: 82.5% ⚠
HP needed = 0.53 HP motor
Utilization: 3.5% ✓
Material Power Factor (K) Reference Table
| Material | K Factor (HP·min/in³) | Relative Difficulty | Notes |
|---|---|---|---|
| Aluminum 6061-T6 | 0.28 | Very Easy | Low cutting forces, high MRR possible |
| Aluminum 7075-T6 | 0.32 | Easy | Slightly harder than 6061 |
| Plastics / Composites | 0.35 | Very Easy | Abrasive wear concern, not power |
| Gray Cast Iron | 0.52 | Easy | Abrasive, chip disposal important |
| Free-Machining Steel 12L14 | 0.60 | Easy | Best steel for MRR efficiency |
| Copper / Brass | 0.90 | Moderate | Good machinability, no coolant needed |
| Mild Steel 1018 | 1.00 | Moderate | Baseline reference material |
| Alloy Steel 4140 | 1.10 | Moderate | Common toolroom steel |
| Ductile Iron | 0.80 | Moderate | Tougher than gray iron |
| Stainless 304 | 1.30 | Difficult | Work hardens — maintain feed |
| Stainless 316 | 1.50 | Difficult | More abrasion resistant than 304 |
| Stainless 17-4 PH | 1.60 | Difficult | Age-hardened — use sharp tooling |
| Hardened Steel 40-50 HRC | 1.40 | Very Difficult | CBN or ceramic tooling recommended |
| Hardened Steel 50-60 HRC | 1.70 | Extreme | Hard milling only, very light cuts |
| Titanium Ti-6Al-4V | 2.00 | Extreme | Heat buildup critical, flood coolant |
| Hastelloy | 2.50 | Extreme | Nickel superalloy, very low SFM |
| Inconel 718 | 3.50 | Extreme | Highest power demand of common alloys |
Frequently Asked Questions
Related CNC Calculators
Top Picks for CNC Router Tooling
Professional-grade carbide tools ready to ship. Click any product to view details and pricing.
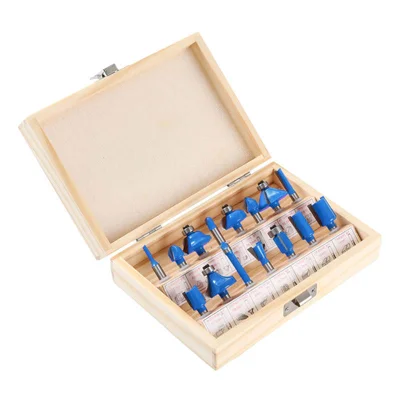
15-Piece Router Bit Set
Multi-size starter kit with carrying case
View on Alibaba →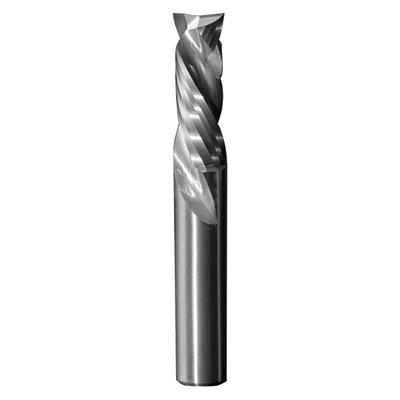
Compression Spiral Bits
Clean edges on plywood & MDF
View on Alibaba →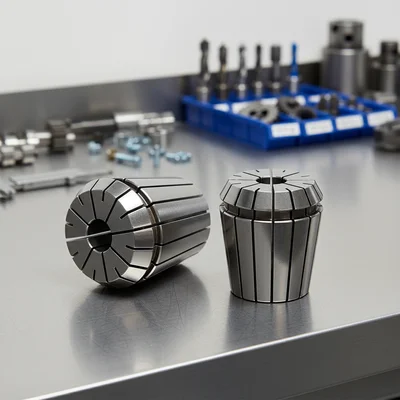
ER Collet Set
Precision holding, zero runout
View on Alibaba →As an Alibaba affiliate partner, we earn from qualifying purchases at no cost to you.